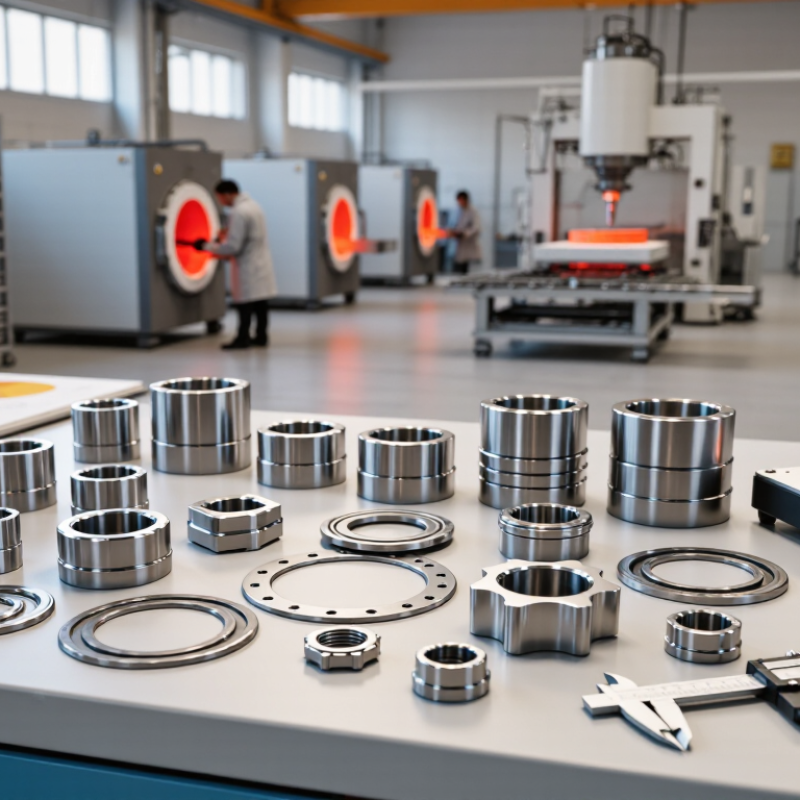
Selecting a reliable ODM Ring Joint Gasket Supplier requires more than comparing prices or browsing polished catalogs. Global buyers need evidence of manufacturing experience, material control, and consistent dimensional accuracy. A gasket may look simple, yet a small deviation in ovality, hardness, or groove fit can affect sealing performance under demanding conditions.
This guide examines leading suppliers through practical purchasing criteria. These include forged material options, heat-treatment records, PMI testing, surface-finish control, and inspection reports. It also considers production capacity, drawing support, packaging quality, and communication across time zones. Experienced suppliers should understand applications involving refineries, petrochemical equipment, offshore systems, and high-pressure process lines. Standards such as API 6A and ASME B16.20 may guide product selection, but buyers must confirm the exact specification for each flange and service condition.
Details matter. Ask for heat numbers. Request dimensional records. Check whether certificates match the delivered batch. A supplier with responsive engineers can resolve tolerance questions before production begins. That saves time.
No supplier list is permanently perfect. Factories change equipment, subcontract processes, or update certifications. Some impressive websites reveal little about actual inspection discipline. Buyers should independently verify current documents, sample quality, lead times, and export experience. A useful comparison also includes communication honesty, not only technical language. The strongest ODM Ring Joint Gasket Supplier is the partner that identifies limitations early, documents every critical step, and improves when a previous assumption proves wrong. That practical caution supports safer sourcing and more dependable long-term purchasing decisions.
Ring joint gaskets create a metal-to-metal seal inside specially machined flange grooves. Their oval or octagonal cross-section concentrates contact pressure along a narrow line. This design suits high-pressure oil, gas, petrochemical, and power-generation equipment. API 6A specifications include working pressure classes from 2,000 to 20,000 psi, where ordinary soft gaskets may not provide enough stability. ASME B16.20 also defines dimensions, materials, and identification requirements for metallic gaskets.
Industrial demand remains closely linked to energy infrastructure. The International Energy Agency reported global oil demand at about 103 million barrels per day in its Oil 2024 analysis. That level supports continued maintenance across refineries, pipelines, and wellhead systems. Ring joint gaskets are commonly manufactured from stainless steel, nickel alloys, or softer metals, depending on temperature, pressure, and chemical exposure. Material selection matters.
An experienced ODM supplier should verify flange standards, groove condition, hardness, coating, and traceability before production. A gasket that is too hard may damage the flange. One that is too soft may deform during tightening. Installation also requires controlled bolt loading and clean sealing surfaces. In practice, errors still occur when buyers treat the gasket as a simple metal ring. That assumption is worth challenging. Supplier documentation should include inspection records, dimensional reports, material certificates, and pressure-test evidence, although documentation alone cannot replace correct installation.
Top ODM Ring Joint Gasket Suppliers for Global Buyers
Choosing an ODM ring joint gasket supplier requires more than comparing prices. According to Grand View Research’s 2024 industrial gaskets analysis, the global market is expanding steadily, driven by oil, gas, chemical, and power applications. That growth increases supplier options, but not necessarily supplier quality. Ask for material certificates, dimensional reports, and traceability from raw stock to shipment. A reliable supplier should manufacture against ASME B16.20, API 6A, or the project’s specified standard. Small details matter. Oval and octagonal rings need controlled hardness, accurate pitch diameter, and clean sealing surfaces.
Production evidence is more useful than polished brochures. Check whether the supplier uses calibrated profile gauges, hardness testers, and documented inspection plans. ISO 9001 certification supports process control, but it does not prove every gasket will perform correctly. Request sample inspection records, batch numbers, and independent test results when the service is critical. The supplier should also explain how it manages stainless steel, nickel alloys, and soft iron without mixing materials. That detail can prevent a costly installation error.
Delivery capability deserves equal attention. Review lead times for tooling, prototypes, and repeat orders. Ask how rejected parts are handled.
A supplier may pass an audit and still miss a practical detail, such as damaged grooves after packaging.
I would not rely on one successful sample. Require a pilot batch, clear acceptance criteria, and technical communication in your working language. Industry data shows continued market growth, yet field reliability still depends on disciplined verification, not optimistic forecasts.
ODM ring joint gasket manufacturing starts with service conditions, not a catalog number. Engineers review pressure, temperature, fluid chemistry, flange class, and installation space. A small error here can become a serious leakage risk.
The design usually follows ASME B16.20 and the relevant API 6A requirements. Engineers select materials such as stainless steel, nickel alloys, or carbon steel. Material choice depends on corrosion exposure and hardness limits. The supplier then converts approved drawings into controlled production data. Forging or bar stock forms the blank. CNC turning creates the oval or octagonal sealing profile. Grooves must remain smooth and accurate. Even minor tool wear can affect contact pressure.
Inspection is practical and traceable. Technicians verify dimensions, surface finish, hardness, material certificates, and heat numbers. Many buyers also request PMI testing, coating checks, and inspection reports. According to Grand View Research’s Industrial Gaskets Market report, the global market was estimated at about USD 13 billion in 2023, with growth expected through 2030. This expansion increases demand for repeatable custom production, not only lower prices. ASME PCC-1-2022 also emphasizes controlled bolting practices, because gasket quality alone cannot correct uneven bolt loading. That point is often underestimated. A perfect gasket can still fail after poor installation. Good ODM work therefore includes drawing review, sample approval, batch inspection, and feedback from field performance. Some specifications remain unnecessarily conservative, but that caution can protect equipment when operating data is incomplete.
A practical reference table for evaluating ODM ring joint gasket capability, engineering requirements, manufacturing controls, and export documentation without identifying individual companies or brands.
| Evaluation Dimension | Industry-Recognized Specification or Practice | ODM Design and Manufacturing Requirement | Typical Evidence from a Qualified Supplier | Buyer Checkpoint |
|---|---|---|---|---|
| 1. Product Design and Application Fit | ||||
| Gasket profile | Common metallic ring joint profiles include Type R, Type RX, and Type BX. | The profile must match the groove geometry, flange design, pressure class, and applicable piping or wellhead specification. | Dimensioned profile drawing, cross-section detail, and application guide. | Confirm profile compatibility |
| Standard reference | ASME B16.20 covers metallic gaskets for pipe flanges, while API 6A is commonly referenced for wellhead and Christmas-tree equipment. | The supplier should identify the governing standard and clearly separate standard dimensions from customer-specific requirements. | Standard reference list, technical datasheet, and compliance statement. | Check the latest applicable edition. |
| Nominal size and pressure class | Ring joint gaskets are manufactured for specific nominal pipe sizes and flange pressure ratings; dimensions are not interchangeable across all classes. | Design input should include nominal size, pressure class, flange or equipment drawing, groove dimensions, and operating conditions. | Approved drawing showing pitch diameter, ring width, height, and tolerances. | Match the gasket to the exact groove. |
| Operating temperature | Temperature capability depends on the selected alloy, process medium, pressure, and service environment. | Material selection should consider minimum and maximum operating temperature, thermal cycling, oxidation, and corrosion exposure. | Material recommendation and temperature-service assessment. | Review the complete pressure-temperature envelope. |
| Process medium | Oil, gas, steam, sour service, hydrogen-containing service, and corrosive chemicals may require different alloys and controls. | The ODM supplier should evaluate chemical compatibility, leakage risk, corrosion mechanisms, and any sour-service requirements before production. | Application questionnaire, material suitability statement, and technical review record. | State the medium and contaminants in the RFQ. |
| 2. Material Selection and Traceability | ||||
| Typical material families | Carbon steel, stainless steel, duplex stainless steel, nickel alloys, and other corrosion-resistant alloys may be used depending on service. | The selected material must provide adequate strength, corrosion resistance, hardness control, and compatibility with the flange material. | Material comparison sheet and approved material specification. | Do not select material by temperature alone. |
| Material standards | Forged ring materials are commonly specified through ASTM or equivalent national and international material standards. | The purchase specification should define the material grade, heat-treatment condition, chemical limits, mechanical requirements, and acceptable substitutions. | Material test certificate with heat number and standard designation. | Verify the certificate against the order. |
| Sour-service requirements | Hydrogen sulfide service can require controls based on NACE MR0175/ISO 15156 or another project-specific sour-service specification. | Hardness, heat treatment, material chemistry, and environmental limits must be reviewed together rather than treated as separate checks. | Hardness report, heat-treatment record, and sour-service compliance declaration. | Confirm the exact project revision and service category. |
| Heat traceability | Metallic pressure-sealing components should be traceable to the original material heat whenever required by the purchase specification. | The heat number should remain linked from incoming material through machining, inspection, packing, and final documentation. | Heat-number log, material certificate, and product identification record. | Require traceability on the inspection plan. |
| 3. ODM Manufacturing Process | ||||
| Engineering review | ODM production should begin with review of drawings, standards, tolerances, service conditions, and inspection requirements. | Conflicting requirements should be resolved before tooling, material purchasing, or batch production. | Contract review form, clarification log, and approved technical drawing. | Approve before production |
| Raw-material preparation | Forged or bar-stock material is selected according to the approved grade and manufacturing route. | Incoming material is checked for identification, dimensions, surface condition, and certificate consistency before machining. | Incoming inspection report and material certificate review. | Reject unidentified or mixed heat material. |
| Machining | CNC turning and precision machining are commonly used to produce the ring profile and sealing surfaces. | Machining programs should control groove-contact geometry, ring dimensions, surface finish, and edge condition. | Process route, CNC inspection record, and first-article report. | Review critical dimensions, not only overall diameter. |
| Heat treatment | Heat treatment may be required by the material specification or service requirement. | Temperature, holding time, cooling method, batch identity, and hardness results should be recorded where applicable. | Heat-treatment chart, furnace record, and hardness report. | Confirm that the treatment applies to the supplied heat. |
| Surface treatment and coating | Metallic ring joint gaskets may be supplied bare or with a specified coating, plating, or surface finish. | Any coating must be compatible with the operating medium, temperature, storage period, and flange-sealing function. | Coating specification, thickness record, and visual inspection report. | Specify whether coating is required or prohibited. |
| 4. Inspection and Quality Assurance | ||||
| Dimensional inspection | Critical ring dimensions must be checked against the approved drawing and applicable standard. | Inspection should include pitch diameter, cross-sectional dimensions, height, width, ovality, and other project-defined characteristics. | Dimensional inspection report with calibrated instrument identification. | Require recorded values, not only a pass statement. |
| Surface condition | Sealing surfaces should be free from harmful cracks, laps, seams, dents, burrs, and unacceptable machining marks. | Visual inspection and, when specified, surface examination should be performed before final packing. | Visual inspection checklist and surface examination report. | Define acceptance criteria in the purchase order. |
| Non-destructive examination | Liquid penetrant, magnetic particle, ultrasonic, or other examinations may be required according to material and project risk. | The examination method must suit the alloy and detect the discontinuity types relevant to the component. | NDE procedure, examiner qualification record, and test report. | Specify method, coverage, and acceptance level. |
| Hardness verification | Hardness control is particularly important for sour-service applications and some project specifications. | Test location, method, frequency, and acceptance limit should be defined by the governing material or service specification. | Hardness map or batch hardness report. | Ensure the limit is project-specific. |
| Quality management | An ISO 9001-based quality management system is commonly used to control documented manufacturing processes. | The supplier should demonstrate control of nonconforming product, calibration, corrective action, document revision, and subcontracted processes. | Quality certificate, calibration list, corrective-action procedure, and audit records. | Verify certificate validity and scope. |
| 5. Packaging, Documentation, and Global Supply | ||||
| Identification marking | Marking commonly includes size or profile information, material grade, heat or batch reference, and traceability code when required. | Markings must remain legible without damaging the sealing surface or creating an unacceptable stress concentration. | Marking photograph, packing list, and traceability register. | Approve marking format before shipment. |
| Packaging | Ring joint gaskets should be protected from impact, moisture, contamination, and corrosion during storage and transport. | Individual separation, protective wrapping, rigid cartons or crates, and desiccant may be used according to material and shipping conditions. | Packaging specification and pre-shipment photographs. | Prevent metal-to-metal damage during transit. |
| Export documentation | Typical documents include commercial invoice, packing list, certificate of origin where required, material certificates, and inspection records. | Document packages should use consistent part numbers, quantities, heat numbers, and revision references. | Sample document index and controlled final dossier. | Agree document requirements before order placement. |
| ODM sample approval | For a new design or modified profile, first-article approval reduces the risk of repeated production errors. | The supplier should submit a sample, drawing, inspection report, and material evidence before full-scale production. | First-article inspection report and signed approval record. | Use for new designs |
| Lead-time planning | Lead time depends on material availability, forging or bar-stock route, heat treatment, machining load, inspection scope, and documentation. | Suppliers should provide a milestone schedule rather than a single unqualified delivery date. | Production schedule covering material, machining, inspection, packing, and dispatch. | Separate standard items from custom ODM items. |
| Supplier comparison method | A qualified supplier should be evaluated on technical capability, traceability, inspection discipline, communication, and total delivered cost. | Use a weighted scorecard instead of selecting solely on unit price. | Completed supplier questionnaire, audit result, and quotation comparison. | Prioritize sealing reliability and documentation. |
Global buyers should judge ODM ring joint gasket suppliers by test evidence, not polished catalogs. ASME B16.20 defines key dimensions, materials, and marking requirements for metallic gaskets. API Specification 6A also supports controlled requirements for pressure-containing equipment and sealing components. Each gasket should carry a heat number, material grade, size, pressure class, and inspection record. Simple traceability prevents a costly mix-up at the warehouse.
Testing must match the service environment. PMI confirms alloy chemistry, while hardness testing helps detect unsuitable heat treatment. Dimensional checks should verify pitch diameter, height, ovality, and surface finish. Pressure or helium leak testing may expose sealing problems that visual inspection misses. The AMPP IMPACT study estimated global corrosion costs at 3.4% of GDP, or about US$2.5 trillion annually. That figure explains why material control deserves serious attention. The ISO Survey 2022 recorded more than 1.2 million ISO 9001 certificates worldwide, yet certification alone cannot prove gasket performance. It is only a framework. Ask for batch-level reports, calibration records, sampling plans, and nonconformance history. Do not accept “tested” without test conditions. A supplier may pass dimensional inspection and still fail during thermal cycling. That possibility is often ignored. Personally, I would also request retained samples and independent verification for critical orders. It adds time, but rushed confidence is not quality.
Global buyers should verify ring joint gasket dimensions, materials, pressure-service suitability, traceability, and quality-system controls against the standards relevant to the purchase. The chart shows the publication year of widely referenced standards used for design, manufacturing, inspection, and material selection. Edition status and project-specific requirements should be confirmed before ordering.
Reference standards: ASME B16.20:2023 for metallic gaskets, API Specification 6A:2018 for wellhead and tree equipment interfaces, ISO 10423:2022 for petroleum and natural gas drilling and production equipment, ISO 9001:2015 for quality management systems, and ISO 15156:2020 for materials in H₂S-containing environments.
Ordering an ODM ring joint gasket requires more than comparing unit prices. Buyers should confirm flange size, pressure class, ring number, material, and required standard. Small dimensional errors can prevent proper seating and delay installation. Request a drawing before production. An experienced supplier should provide material certificates, hardness results, inspection records, and clear revision control. These documents support technical review and reduce disputes across borders. Ask about minimum order quantities, sample charges, tooling ownership, and approval timelines. Custom solutions may change machining steps, packaging, and delivery dates. Do not accept vague promises.
For demanding services, specify alloy grade, coating needs, temperature range, and media exposure. Ring gaskets need controlled hardness to protect flange faces and maintain sealing performance. However, material selection should follow actual process conditions, not a generic catalog recommendation. That distinction matters. An ODM partner can adjust cross-section, tolerances, marking, and packing after drawing approval. Keep every change in writing. One overlooked revision can create mixed inventory. Pilot orders and dimensional inspection are sensible, especially with unfamiliar suppliers. Not every first sample will be perfect.
International supply planning needs realistic lead times, not optimistic factory estimates. Confirm production capacity, holiday closures, payment terms, Incoterms, and destination-port responsibilities. Export cartons should resist moisture, while labels should match purchase documents and customs descriptions. Ask for heat numbers and batch traceability on every lot. Freight delays happen. Buffer stock can protect shutdown-sensitive projects. A cheaper quote may become expensive after rework, storage, or emergency freight. Review supplier communication during sampling, not only after ordering. Confidence is earned slowly.
Copyright © 2025 The Toolroom Inc. All Rights Reserved.
Website Design St Louis by IQComputing